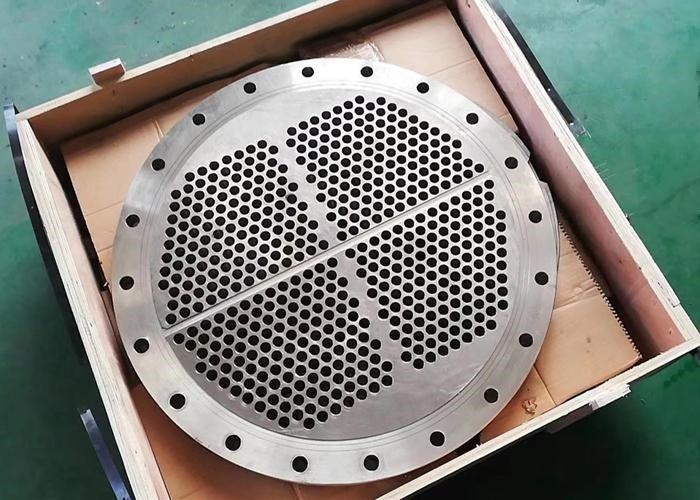
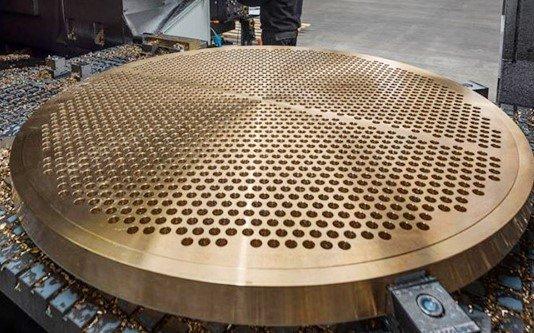
Carbon Steel and Clad Tube Sheets
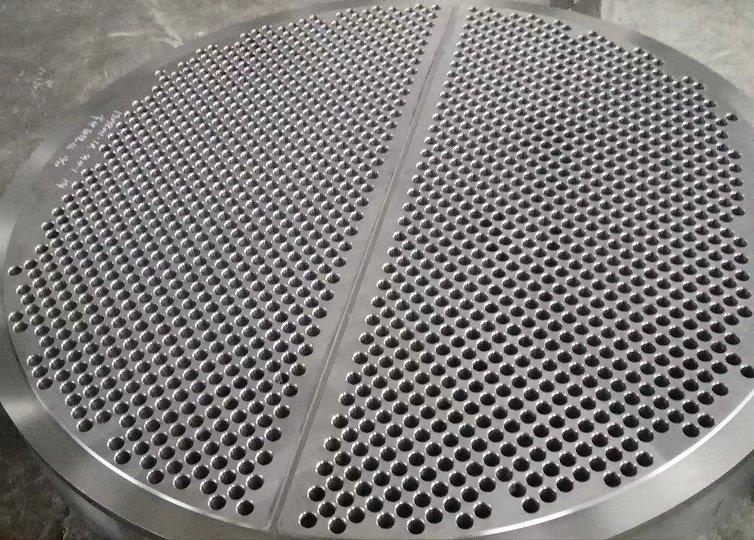
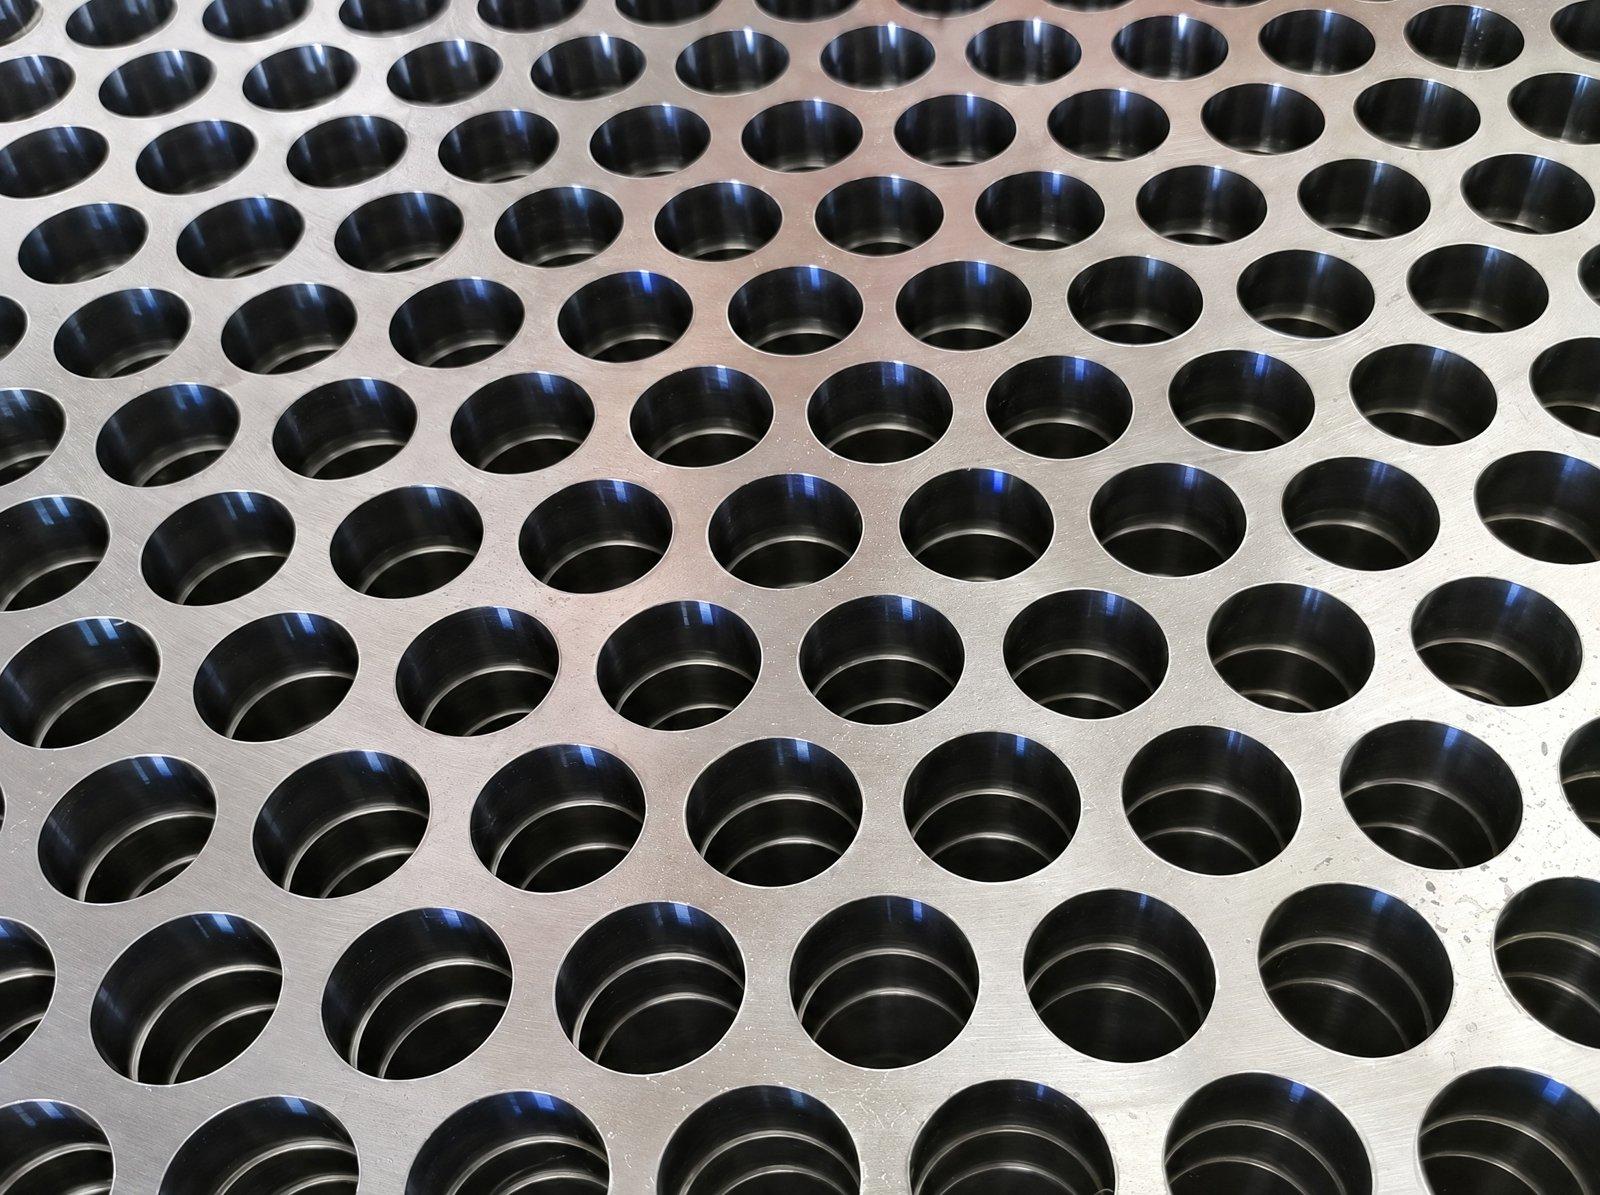
Tube sheets in SA-516-70 plate and SA-266, SA-105, SA-350 LF2 and SA-182 forgings, plain or explosion-clad and weld-overlaid, drilled, grooved and finished to your drawing and TEMA. Made to TEMA (10th ed. / 2026 ed.), ASME VIII Div 1 (Part UHX), ASTM A516. Supplied from Dubai with an Indus part number for each size and mill test certificates on request.
Key features
- Product type: Carbon Steel and Clad Tube Sheets
- Construction: Machined from plate or forging to your drawing
- Standards: TEMA (10th ed. / 2026 ed.), ASME VIII Div 1 (Part UHX), ASTM A516, ASTM A266, ASTM A105, ASTM A350, ASTM A182, ASTM A240, ASTM A263, ASTM A264
- Product type
- Carbon Steel and Clad Tube Sheets
- Construction
- Machined from plate or forging to your drawing
Product description
Tube sheets in SA-516-70 plate and SA-266, SA-105, SA-350 LF2 and SA-182 forgings, plain or explosion-clad and weld-overlaid, drilled, grooved and finished to your drawing and TEMA.
Specification
- Product form by thickness: Plate (SA-516-70) for thinner sheets; forged discs (SA-266, SA-105, SA-350 LF2, SA-182) above about 100-125 mm or for high-integrity service
- Low-temperature tubesheet material: SA-350 LF2 forging for low-temperature service (about -46 to -48 C); SA-516-70 may need normalizing and impact testing by thickness/MDMT (UCS-66)
- SA-516-70 tensile / yield: 485-620 MPa tensile; 260 MPa min yield; elongation 21% (50 mm) / 17% (200 mm)
- SA-516-70 normalizing: Plates over 38 mm (1.5 in) supplied normalized unless otherwise ordered
- Cladding options: Explosion-clad (SS 304L/316L, duplex 2205/2507, Ti Gr1/2, alloy 625/825/C-276, Cu-Ni 90/10 or 70/30 on SA-516-60/70 or P265GH/P355GH) or weld overlay
- Explosion-clad layer thickness: 3-10 mm typical for tube sheets; 1-50 mm possible; base 10-500 mm; single pieces to about 50 t; flatness within 1 mm/m
- Clad bond inspection: 100% UT of bond per ASME SA-263 / SA-264 / SA-265 (or EN 13445-2), including after simulated PWHT
- Explosion clad vs weld overlay: Explosion clad keeps full alloy chemistry (no dilution) and the full clad thickness is drillable and weldable; overlay adds dilution, heat input and distortion and suits small or one-off parts
- Clad tubesheet strength welds: ASME VIII Div 1 UW-20.7 lets tube-to-tubesheet welds in integral clad be strength welds if shear test and UT are done
- Minimum tube pitch: 1.25 x tube OD (triangular or square)
- Square-pitch cleaning lane (mechanical cleaning): min 6.4 mm (1/4 in); 4.8 mm (3/16 in) allowed in shells <= 12 in (Class C)
- Class C pitch exception: 1.2 x OD permitted for tubes 5/8 in and smaller with expanded joints
- Tube layout angles: 30 deg (triangular), 60 deg (rotated triangular), 90 deg (square), 45 deg (rotated square)
- Tubesheet hole, standard fit, 3/4 in (19.05 mm) tube: 0.760 in (19.30 mm) nominal, under-tolerance 0.004 in (0.10 mm)
- Tubesheet hole, standard fit, 1 in (25.4 mm) tube: 1.012 in (25.70 mm) nominal, under-tolerance 0.004 in (0.10 mm)
- Tube-hole clearance in practice: Drill and ream to 0.007-0.010 in (0.18-0.25 mm) over tube OD (heat exchangers and condensers); boiler drum / header seats about 1/32 in (0.8 mm) over OD
- Special close fit holes: Mandatory in ACHE headers when tubes are austenitic SS, duplex SS, titanium, copper-nickel or nickel alloy (ISO 13706 / API 661 cl. 9.3.1.2)
- Tube-hole grooving (expanded joints): Grooves for tubes 5/8 in OD and larger; 1 groove when tubesheet <= 25 mm (1 in) thick, 2 grooves when thicker; grooves about 3.2 mm (1/8 in) wide with 6.4 mm (1/4 in) between them; final size/arrangement at maker's discretion
Standards
TEMA (10th ed. / 2026 ed.), ASME VIII Div 1 (Part UHX), ASTM A516, ASTM A266, ASTM A105, ASTM A350, ASTM A182, ASTM A240, ASTM A263, ASTM A264, ASTM A265, API 660 / API 661, EN 13445-3, ASTM A387, EN 1092-1. Equivalent grades across ASTM, EN, DIN, JIS and GB/T standards are indicative; we check them against each tender.
Testing and documents
- Clad bond 100% UT (SA-263/264/265)
- Hydrotest of the completed exchanger
- Tube-to-tubesheet procedure qualification (purchaser approval under API 661)
- Mill test certificate to EN 10204 3.1 on request; third-party inspection can be arranged against your inspection and test plan
Where it is used
- Feedwater heaters and condensers in power plants
- Refinery and gas-plant shell-and-tube exchangers (T&I replacement tube sheets)
- Seawater coolers and desalination (clad duplex / Ti / Cu-Ni)
Standard geometry
| Tube OD (in) | Tube OD (mm) | Min pitch 1.25 x OD (in) | Min pitch 1.25 x OD (mm) | Min square pitch with 6.4 mm (1/4 in) cleaning lane (in) | Min square pitch with cleaning lane (mm) |
|---|---|---|---|---|---|
| 5/8 | 15.88 | 0.781 | 19.84 | 0.875 | 22.23 |
| 3/4 | 19.05 | 0.938 | 23.81 | 1.000 | 25.40 |
| 1 | 25.40 | 1.250 | 31.75 | 1.250 | 31.75 |
| 1-1/4 | 31.75 | 1.563 | 39.69 | 1.563 | 39.69 |
| 1-1/2 | 38.10 | 1.875 | 47.63 | 1.875 | 47.63 |
These are the limits of the standard, not part numbers. Each item is made to your drawing.
How we supply
Tube sheets, baffles and plates are made to the purchaser's drawing, so there is no catalogue part number for each size. We cut, machine, drill, ream and groove them from certified plate or forgings, stack-drill baffles and support plates so the holes line up through the bundle, and check hole size, pitch and ligaments against the drawing before dispatch. Send the drawing, or the material, the outside diameter, the thickness, the tube size and the pitch and layout, and we quote with the mill certificates and the inspection you need.
Ordering
Quote the Indus part number from the size table, or send the standard and grade, the outside diameter and wall (BWG or millimetres, minimum or average wall), the length and the quantity. We quote with the mill certificates and the inspection you need.
Identification
| Parameter | Value |
|---|---|
| Product type | Carbon Steel and Clad Tube Sheets |
| Construction | Machined from plate or forging to your drawing |
Compliance
| Parameter | Value |
|---|---|
| Standards | TEMA (10th ed. / 2026 ed.), ASME VIII Div 1 (Part UHX), ASTM A516, ASTM A266, ASTM A105, ASTM A350, ASTM A182, ASTM A240, ASTM A263, ASTM A264 |
Dimensions
| Parameter | Value |
|---|---|
| Length | Random or fixed lengths; cut to length on request |
| Size table | Made to your drawing; standard geometry in the description |
Quality
| Parameter | Value |
|---|---|
| Testing | Clad bond 100% UT (SA-263/264/265); Hydrotest of the completed exchanger; Tube-to-tubesheet procedure qualification (purchaser approval under API 661) |
| Certification | Mill test certificate to EN 10204 3.1 on request; third-party inspection by arrangement |
Application
| Parameter | Value |
|---|---|
| Typical services | Feedwater heaters and condensers in power plants; Refinery and gas-plant shell-and-tube exchangers (T&I replacement tube sheets); Seawater coolers and desalination (clad duplex / Ti / Cu-Ni) |
Shipping & lead time
What are carbon Steel and Clad Tube Sheets used for?▾
How do I order the Carbon Steel and Clad Tube Sheets when there is no size table?▾
What is the minimum tube pitch for the Carbon Steel and Clad Tube Sheets?▾
How thick is the explosion-clad layer on a tube sheet?▾
What are the tube hole and expansion details for the Carbon Steel and Clad Tube Sheets?▾
Which materials are the Carbon Steel and Clad Tube Sheets made from?▾
Which standards and certificates apply to the Carbon Steel and Clad Tube Sheets?▾
What goes with the Carbon Steel and Clad Tube Sheets in an exchanger?▾
What testing applies to the Carbon Steel and Clad Tube Sheets?▾
How do the Carbon Steel and Clad Tube Sheets compare with other tube sheet materials?▾
Can you export the Carbon Steel and Clad Tube Sheets from Dubai?▾
Do you keep the Carbon Steel and Clad Tube Sheets in stock in Dubai?▾
Shipped worldwide from our Dubai warehouse. Transit, routes and documentation for 136 destinations
From the blog