
Studded Tubes
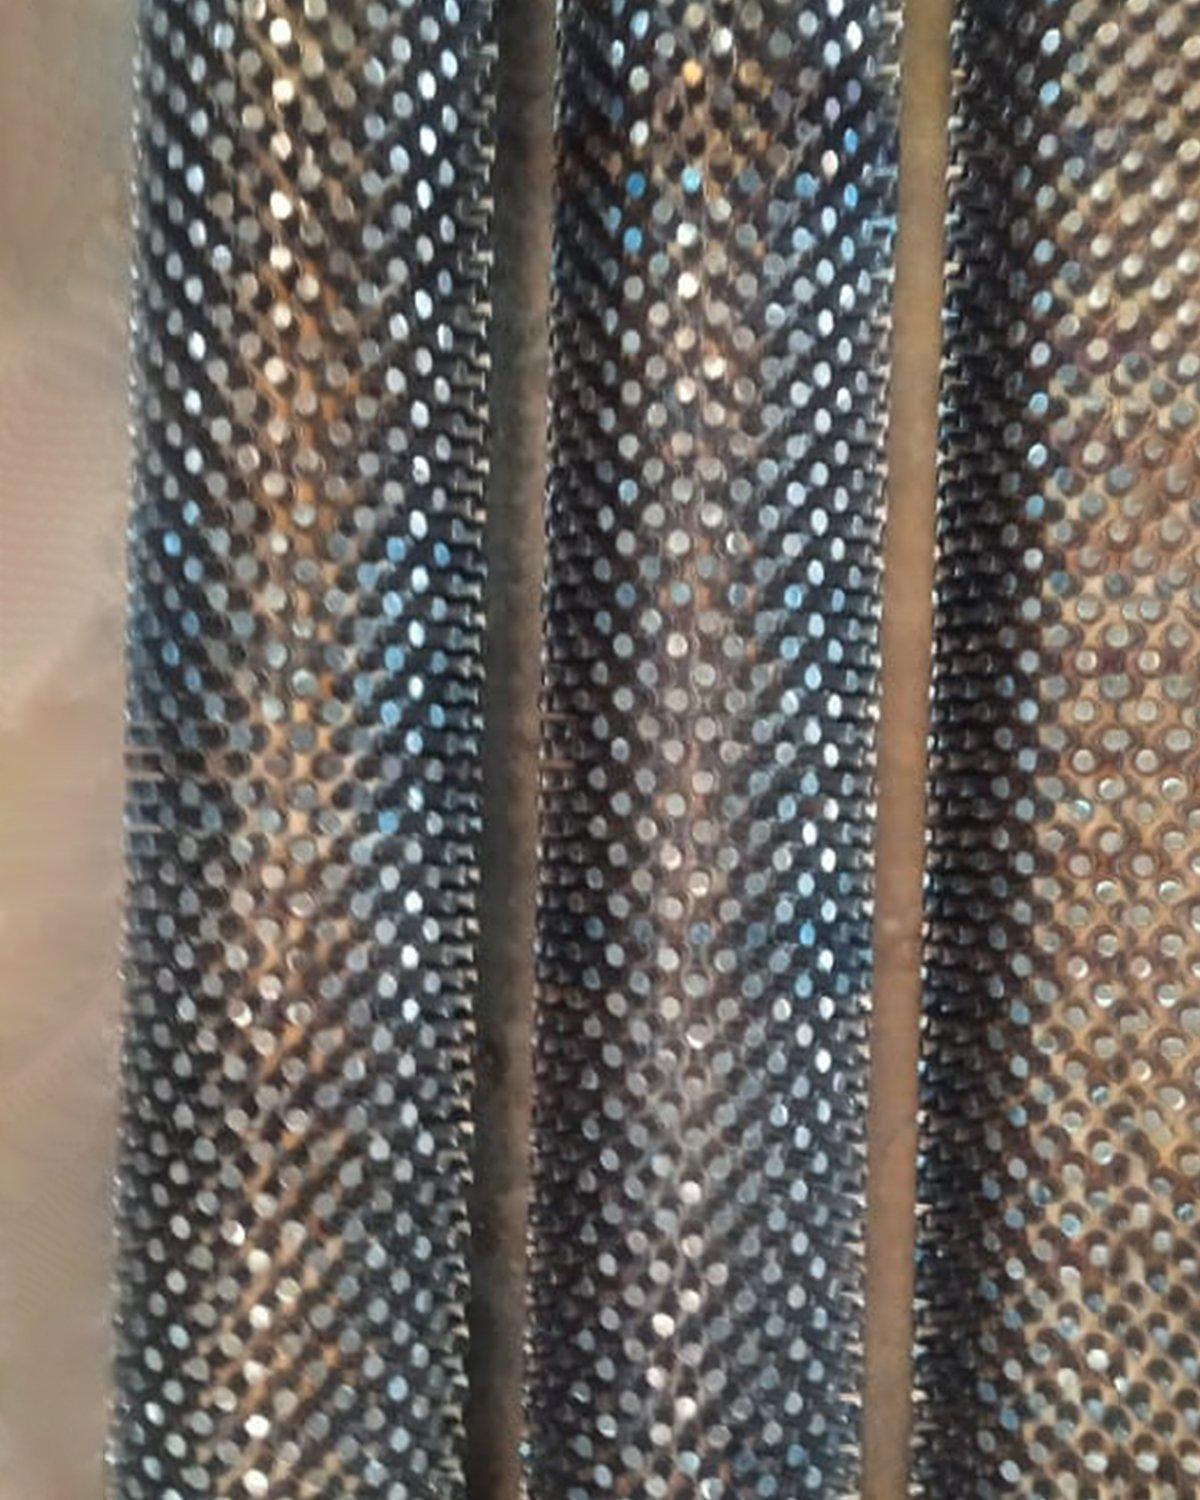
Steel studs welded in rows round the tube, for fired-heater convection sections. Made to API 560, ASTM A106, ASTM A335. Supplied from Dubai with an Indus part number for each size and mill test certificates on request.
Key features
- Product type: Studded Tubes
- Construction: Each stud arc- or resistance-welded to the tube
- Standards: API 560, ASTM A106, ASTM A335, ASTM A312, ASTM A192, ASTM A193, ASTM A199, ASTM A213, ASTM A510
- Base tube material: A106 B; A335 P5/P9; A213 T9; A312 TP347
- Fin material: CS studs; 11–13Cr; 18Cr-8Ni; 25Cr-20Ni
- Maximum service temperature: Set by stud material; fired-heater stud-tip limits per API 560: carbon steel 454 °C, 2¼Cr / 5Cr 549 °C, 25Cr-20Ni 982 °C
- Product type
- Studded Tubes
- Construction
- Each stud arc- or resistance-welded to the tube
- Base tube material
- A106 B; A335 P5/P9; A213 T9; A312 TP347
- Fin material
- CS studs; 11–13Cr; 18Cr-8Ni; 25Cr-20Ni
Product description
Steel studs welded in rows round the tube, for fired-heater convection sections. Studs shed soot and ash better than fins, so they are used on the shield rows and where the burners fire liquid or dirty fuel.
Specification
- Maximum service temperature: Set by stud material; fired-heater stud-tip limits per API 560: carbon steel 454 °C, 2¼Cr / 5Cr 549 °C, 25Cr-20Ni 982 °C
- Stud diameter (mm): 12.7 (1/2 in) most common
- Stud height (mm): 25.4 (1 in) typical; max 19 for heavier liquid fuels
- Stud row spacing (mm): 15.9 (0.625 in), i.e. ~63 rows/m (19.2 rows/ft)
- Attachment: Each stud arc- or resistance-welded to the tube
- Support: At least three rows of studs rest on each tube support
- Where used: Convection section only; three rows of bare shield tubes between extended surface and the radiant firebox
- Fuel rule: Some owner specifications: vertical convection tubes on liquid fuel must use studs, not fins
Standards
API 560, ASTM A106, ASTM A335, ASTM A312, ASTM A192, ASTM A193, ASTM A199, ASTM A213, ASTM A510. Equivalent grades across ASTM, EN, DIN, JIS and GB/T standards are indicative; we check them against each tender.
Materials
- Tube: A106 B; A335 P5/P9; A213 T9; A312 TP347
- Fins: CS studs; 11–13Cr; 18Cr-8Ni; 25Cr-20Ni
Testing and documents
- Stud weld quality per heater spec; base tube hydrotest
- Mill test certificate to EN 10204 3.1 on request; third-party inspection can be arranged against your inspection and test plan
Where it is used
- Refinery crude, vacuum and reformer heater convection sections firing fuel oil or mixed fuel
Sizes
1 size, each under its own Indus part number in the size table. The table lists typical sizes for the range; other sizes are made on request.
Ordering
Quote the Indus part number from the size table, or send the standard and grade, the outside diameter and wall (BWG or millimetres, minimum or average wall), the length and the quantity, with the fin type, material, height, thickness and fins per inch, and the bare length at each end. We quote with the mill certificates and the inspection you need.
Identification
| Parameter | Value |
|---|---|
| Product type | Studded Tubes |
| Construction | Each stud arc- or resistance-welded to the tube |
Compliance
| Parameter | Value |
|---|---|
| Standards | API 560, ASTM A106, ASTM A335, ASTM A312, ASTM A192, ASTM A193, ASTM A199, ASTM A213, ASTM A510 |
Construction
| Parameter | Value |
|---|---|
| Base tube material | A106 B; A335 P5/P9; A213 T9; A312 TP347 |
| Fin material | CS studs; 11–13Cr; 18Cr-8Ni; 25Cr-20Ni |
Dimensions
| Parameter | Value |
|---|---|
| Length | Random or fixed lengths; cut to length on request |
| Size table | Typical sizes — other sizes on request |
Performance
| Parameter | Value |
|---|---|
| Maximum service temperature | Set by stud material; fired-heater stud-tip limits per API 560: carbon steel 454 °C, 2¼Cr / 5Cr 549 °C, 25Cr-20Ni 982 °C |
Quality
| Parameter | Value |
|---|---|
| Testing | Stud weld quality per heater spec; base tube hydrotest |
| Certification | Mill test certificate to EN 10204 3.1 on request; third-party inspection by arrangement |
Application
| Parameter | Value |
|---|---|
| Typical services | Refinery crude, vacuum and reformer heater convection sections firing fuel oil or mixed fuel |
Shipping & lead time
Sizes & part numbers
1 size- Indus part no.IH-TF-ST-STD-R1
- Stud dia. (mm)
- 12.7
- Stud dia. (in)
- 1/2
- Stud height (mm)
- 25.4
- Row spacing (mm)
- 15.9
- Rows per metre
- 63
Stud dia. (mm) — Stud diameter in millimetres. Stud dia. (in) — The same stud diameter in inches. Stud height (mm) — Stud height above the tube surface, in millimetres. Row spacing (mm) — Distance between stud rows along the tube, in millimetres. Rows per metre — Stud rows per metre of studded length.
These are typical sizes for the range, not a full mill list. Other diameters, walls, fin geometries and lengths are made to order: tell us the standard and grade, the O.D. and wall, and the length you need. Mill test certificates to EN 10204 3.1 are available on request.
What are studded tubes used for?▾
How is the part number IH-TF-ST-STD-R1 read?▾
What stud diameter, height and spacing do the studded tubes have?▾
How many rows of studs must rest on each tube support?▾
What is the maximum service temperature of the Studded Tubes?▾
What materials are the Studded Tubes made from?▾
Which standards and certificates apply to the Studded Tubes?▾
Where do studded tubes sit in a fired heater?▾
How are the studs attached and checked on the Studded Tubes?▾
Studs or fins: which suits a fired-heater convection section?▾
Can you export the Studded Tubes from Dubai?▾
Do you keep the Studded Tubes in stock in Dubai?▾
Shipped worldwide from our Dubai warehouse. Transit, routes and documentation for 136 destinations
From the blog
Written about this part
Heat-transfer tubes
HF-welded spiral fin tubes: solid or serrated?
High-frequency welded spiral fins are the workhorse of fired-heater convection sections, HRSGs and economisers. When to choose solid or serrated fins, which fin material for which tip temperature, and when studs or H-fins are the better answer.
3 min read
Heat-transfer tubes
Finned tube fouling and cleaning in Gulf dust
Dust, sand and salt clog air-cooler fins across the Gulf every summer, just when the coolers are working hardest. How fouling builds up on finned tube, how to clean it without flattening the fins, and the design choices that make the next bundle easier to keep clean.
2 min read