
Feedwater Heater U-Tubes
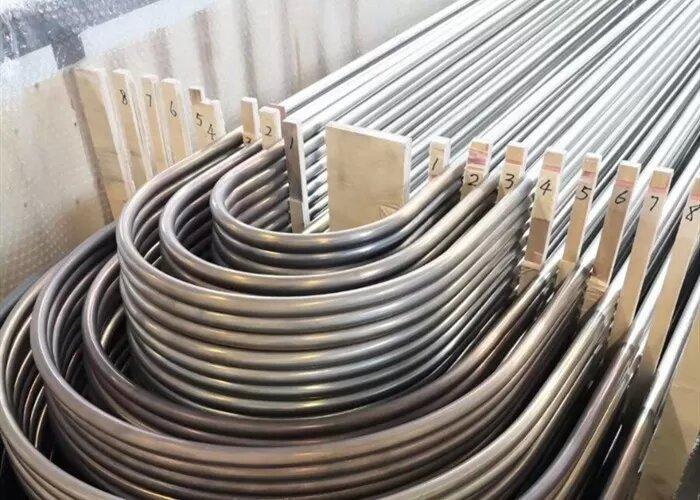
Stainless U-tubes to ASTM A688 and A803 and carbon steel U-tubes to ASTM A556 for high- and low-pressure feedwater heaters in power and desalination plants. Made to ASTM A688, ASTM A556, ASTM A803. Supplied from Dubai with an Indus part number for each size and mill test certificates on request.
Key features
- Product type: Feedwater Heater U-Tubes
- Construction: Bent from straight seamless or welded tube
- Standards: ASTM A688, ASTM A556, ASTM A803
- Base tube material: TP304/304L/304N; TP316/316L; N08367; A556 A2/B2/C2; A803 TP439
- Wall thickness: Per the governing specification on the order (ASTM A688 / TEMA, or A556 / B395) — no single percentage
- Product type
- Feedwater Heater U-Tubes
- Construction
- Bent from straight seamless or welded tube
- Base tube material
- TP304/304L/304N; TP316/316L; N08367; A556 A2/B2/C2; A803 TP439
Product description
Stainless U-tubes to ASTM A688 and A803 and carbon steel U-tubes to ASTM A556 for high- and low-pressure feedwater heaters in power and desalination plants.
Specification
- Minimum bend radius: 1.5×OD centreline radius available; dimensional tolerances guaranteed from 2×OD
- Wall thinning at the bend: Per the governing specification on the order (ASTM A688 / TEMA, or A556 / B395) — no single percentage
- Bend heat treatment: To order: stress-relief or solution anneal of the bend plus ~150 mm of leg (A688), or ≥300 mm where the project specification requires
- Leg length: Up to ~12 m typical; straight tube up to 30 m on request
- A688 tensile TP304/316: 515 MPa / 205 MPa / 35 %
- A688 tensile TP304L/316L: 485 MPa / 175 MPa / 35 %
- A688 hardness: 90 HRB max (XM-29 and N08367: 100 HRB); not applied to un-heat-treated bend area
- A688 welded tube: Automatic weld, no filler; weld (or weld and base) cold worked before final HT; reverse-bend test per 460 m
- A556 grades: A2 / B2 / C2: tensile 320/410/480 MPa; yield 180/260/280 MPa; hardness 72/79/89 HRB
- ASTM A688 scope: A688 scope: Seamless AND welded austenitic FWH tubes, incl. U-tubes; 15.9–25.4 mm (5/8–1 in) OD; average or minimum wall 0.7 mm (0.028 in) and heavier; A688 bend HT: Optional; same solution anneal as straight tube (≥1040 °C, rapid cool below 370 °C; N08367 1107 °C) over bend + ~150 mm per leg; inert ID purge; A688 thinning: t_f ≥ 4RT/(4R + D); A688 ovality: ≤10 % of pre-bend OD at R ≥ 2D; A688 pressure test: Each U-tube after bending/HT: hydro (A1016 or agreed) or pneumatic; A688 chloride limit: Residual chloride on tube surfaces ≤10.7 mg/m² (1 mg/ft²) at packing; one tube per 500 checked; A556 scope: Seamless cold-drawn carbon steel FWH tubes incl. U-tubes; 15.9–31.8 mm (5/8–1-1/4 in) OD; minimum wall ≥1.1 mm (0.045 in); A556 bend stress relief: If specified, heat the bent portion to 585–640 °C (1100–1200 °F); straight tube tempered ≥640 °C after last draw; A556 thinning: t_f ≥ T·2R/(2R + D) — more severe than the A688/TEMA form; A556 ovality and OD tolerance: ≤10 % at R ≥ 2D (1.5D may exceed); straight OD ±0.10 mm under 25.4 mm, ±0.15 mm 25.4–31.7 mm; wall +20/−0 %; A556 hydro: Each U-tube hydro tested (or 1.5 × design pressure by agreement); A803 scope: Ferritic stainless FWH tubes incl. U-tubes, 15.9–25.4 mm OD, wall ≥0.7 mm; straight tube for bending furnished annealed; B395 (copper-alloy U-bends, for comparison): Dual-gage option: central bend section one BWG heavier, ≥100 mm long and ≥ bend arc (+76/−0 mm); thinning t_f ≥ t·2R/(2R + D); ovality ≤10 %; leg spacing ±1.6 mm; Cu-Ni HR50 radius ≥2.2×OD (1.24 mm wall) / ≥2×OD (1.47 mm wall); brass/admiralty bends must be relief annealed, Cu-Ni bends if specified; eddy current before bending
Standards
ASTM A688, ASTM A556, ASTM A803. Equivalent grades across ASTM, EN, DIN, JIS and GB/T standards are indicative; we check them against each tender.
Materials
- Tube: TP304/304L/304N; TP316/316L; N08367; A556 A2/B2/C2; A803 TP439
Testing and documents
- A262 IGC on straight lots and on the smallest heat-treated bend (A688)
- Each U-tube pressure tested after bending
- Each straight tube electric-tested after final HT (A688 §12, A556 §12)
- Optional eddy current S1/S2 with EDM notch standards (A688)
- Mill test certificate to EN 10204 3.1 on request; third-party inspection can be arranged against your inspection and test plan
Where it is used
- Power-plant and cogeneration feedwater heaters (A688 stainless, A556 carbon, A803 ferritic)
Standard geometry
| Standard | OD (mm) | OD (in) | Min wall covered (mm) | Leg tolerance |
|---|---|---|---|---|
| ASTM A688 | 15.88 | 5/8 | 0.7 | +3.2 to 6 m / +4.0 to 9 m / +4.8 to 12.2 m |
| ASTM A688 | 19.05 | 3/4 | 0.7 | same |
| ASTM A688 | 22.23 | 7/8 | 0.7 | same |
| ASTM A688 | 25.40 | 1 | 0.7 | same |
| ASTM A556 | 15.88 | 5/8 | 1.1 | same table |
| ASTM A556 | 19.05 | 3/4 | 1.1 | same table |
| ASTM A556 | 25.40 | 1 | 1.1 | same table |
| ASTM A556 | 31.75 | 1-1/4 | 1.1 | same table |
| ASTM A803 | 15.88–25.40 | 5/8–1 | 0.7 | per A803 (not retrieved) |
These are the limits of the standard, not part numbers. Each item is made to your drawing.
Ordering
Quote the Indus part number from the size table, or send the standard and grade, the outside diameter and wall (BWG or millimetres, minimum or average wall), the length and the quantity, with the bend schedule: centreline radius and leg length for each row, and any heat treatment of the bends. We quote with the mill certificates and the inspection you need.
Identification
| Parameter | Value |
|---|---|
| Product type | Feedwater Heater U-Tubes |
| Construction | Bent from straight seamless or welded tube |
Compliance
| Parameter | Value |
|---|---|
| Standards | ASTM A688, ASTM A556, ASTM A803 |
Construction
| Parameter | Value |
|---|---|
| Base tube material | TP304/304L/304N; TP316/316L; N08367; A556 A2/B2/C2; A803 TP439 |
Dimensions
| Parameter | Value |
|---|---|
| Wall thickness | Per the governing specification on the order (ASTM A688 / TEMA, or A556 / B395) — no single percentage |
| Length | Random or fixed lengths; cut to length on request |
| Bend radius | 1.5×OD centreline radius available; dimensional tolerances guaranteed from 2×OD |
| Size table | Made to your drawing; standard geometry in the description |
Quality
| Parameter | Value |
|---|---|
| Testing | A262 IGC on straight lots and on the smallest heat-treated bend (A688); Each U-tube pressure tested after bending; Each straight tube electric-tested after final HT (A688 §12, A556 §12); Optional eddy current S1/S2 with EDM notch standards (A688) |
| Certification | Mill test certificate to EN 10204 3.1 on request; third-party inspection by arrangement |
Application
| Parameter | Value |
|---|---|
| Typical services | Power-plant and cogeneration feedwater heaters (A688 stainless, A556 carbon, A803 ferritic) |
Shipping & lead time
What are feedwater heater U-tubes used for?▾
What sizes do ASTM A688 and ASTM A556 feedwater heater U-tubes come in?▾
How long can feedwater heater U-tube legs be?▾
How tight a bend radius can feedwater heater U-tubes take?▾
Which grades are available for ASTM A688 and A803 feedwater heater tubes?▾
What tests apply to ASTM A688 feedwater heater U-tubes?▾
Do feedwater heater U-tubes come with mill test certificates?▾
Does the bend of a feedwater heater U-tube need heat treatment?▾
What residual chloride limit applies to A688 feedwater heater tubes when packed?▾
How does A688 stainless feedwater heater tube differ from A556 carbon steel?▾
Where do feedwater heater U-tubes go in a power plant?▾
Can you supply feedwater heater U-tubes from Dubai?▾
Shipped worldwide from our Dubai warehouse. Transit, routes and documentation for 136 destinations
From the blog